
Machining Capability
Precision Engineering for EDC Wallets
TOPWALLET’s engineering team controls every dimension that affects how an EDC wallet feels in the hand, ejects cards, and survives daily use. Whether you are launching a slim card holder or a multi-function money clip, our process is built to hold tight tolerances from the first prototype to the 10,000th unit. Products that leave this process live in the TOPWALLET production catalogue — see the finished designs the process supports.
±0.05 mm
Uniform assembly gaps and smooth card ejection, held on 120+ CNC stations
60+
Engineers across DFM, tooling, and quality teams — your questions answered in hours, not weeks
24 h
DFM report turnaround so your project never stalls waiting on us
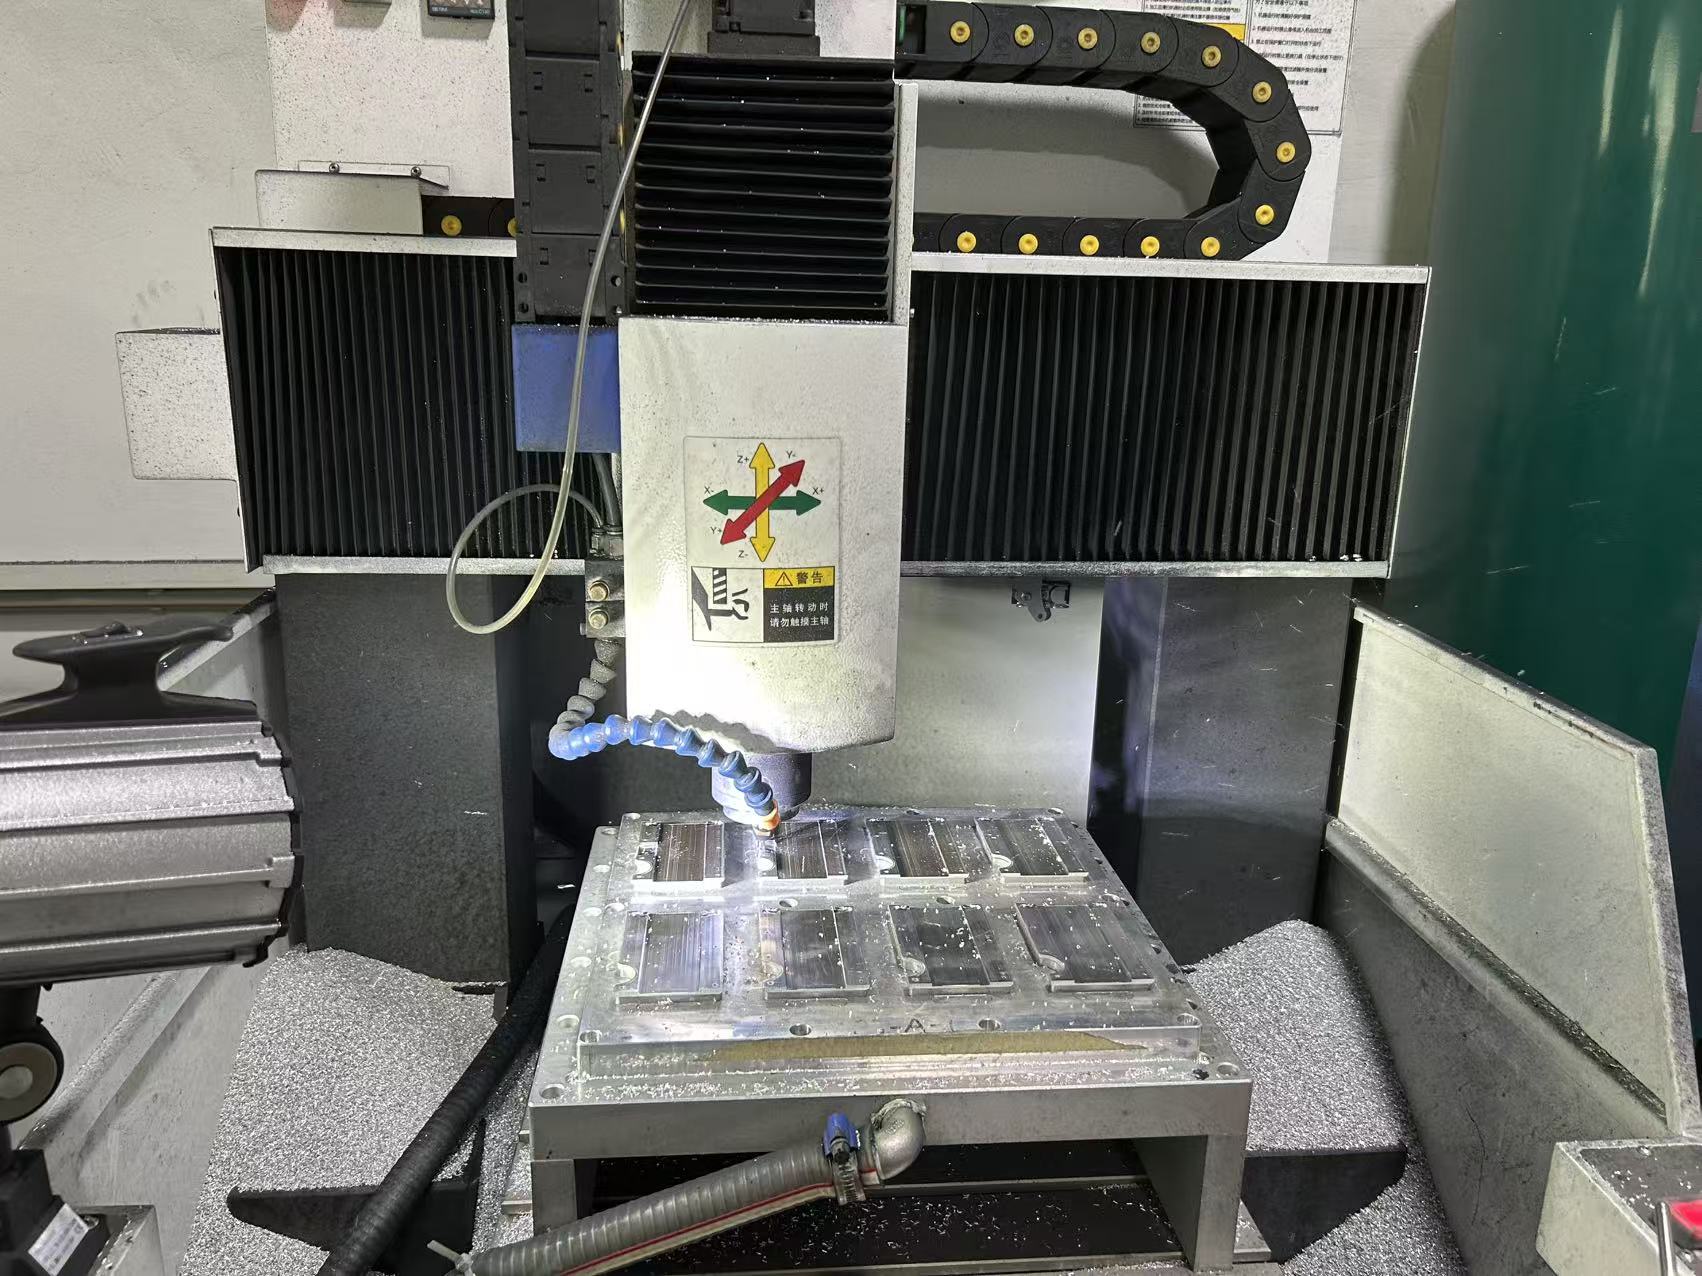
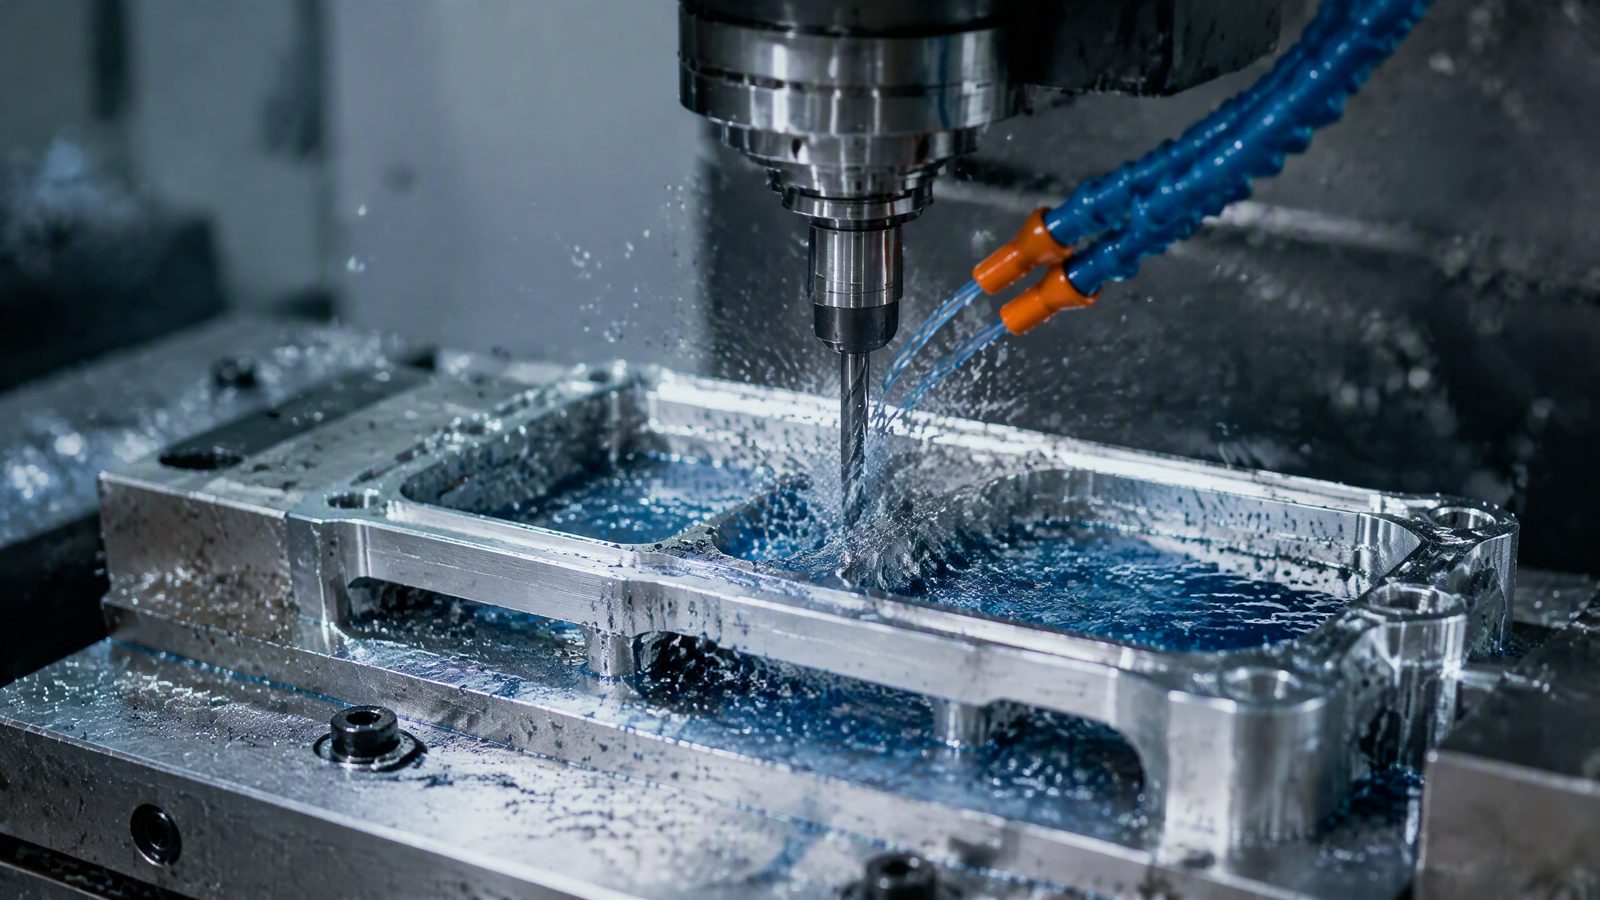
5-axis CNC cell machining a wallet shell — representative of the fleet used for your tooling and production.
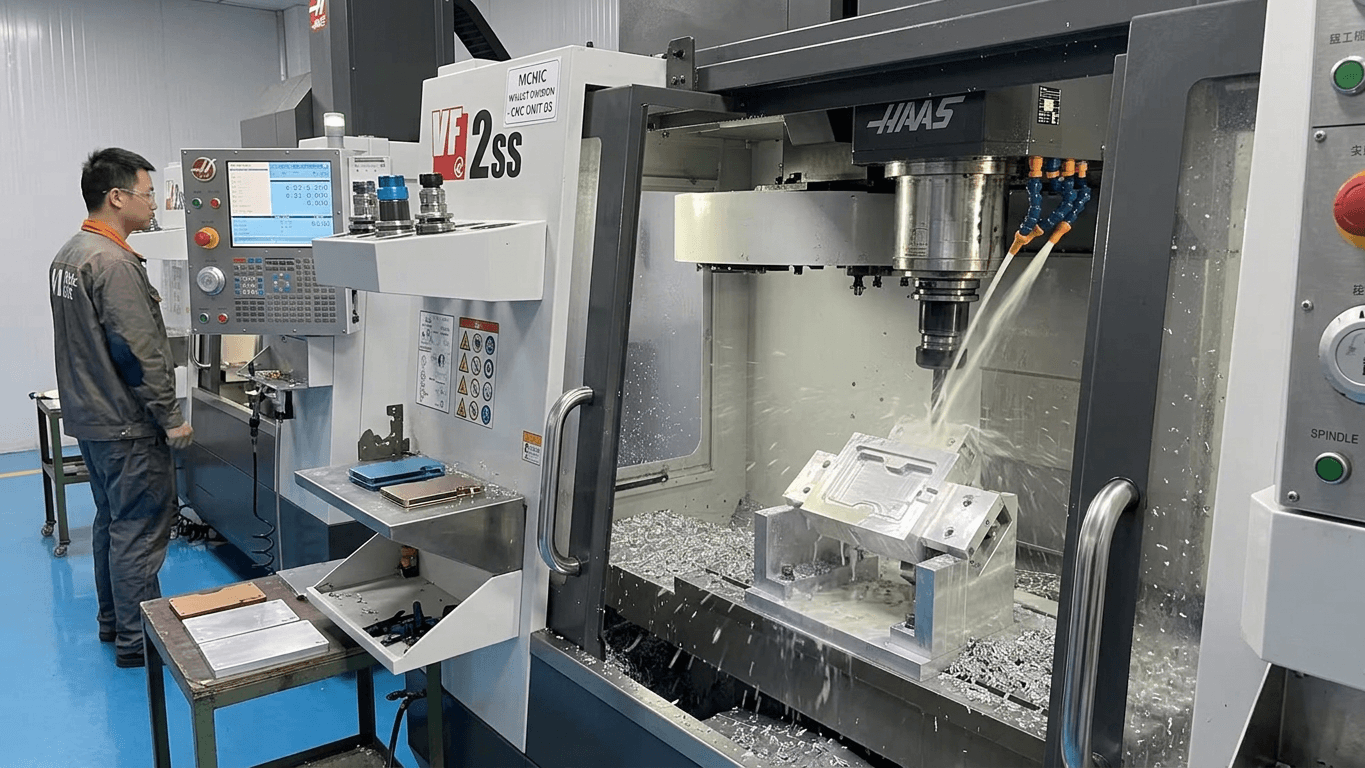
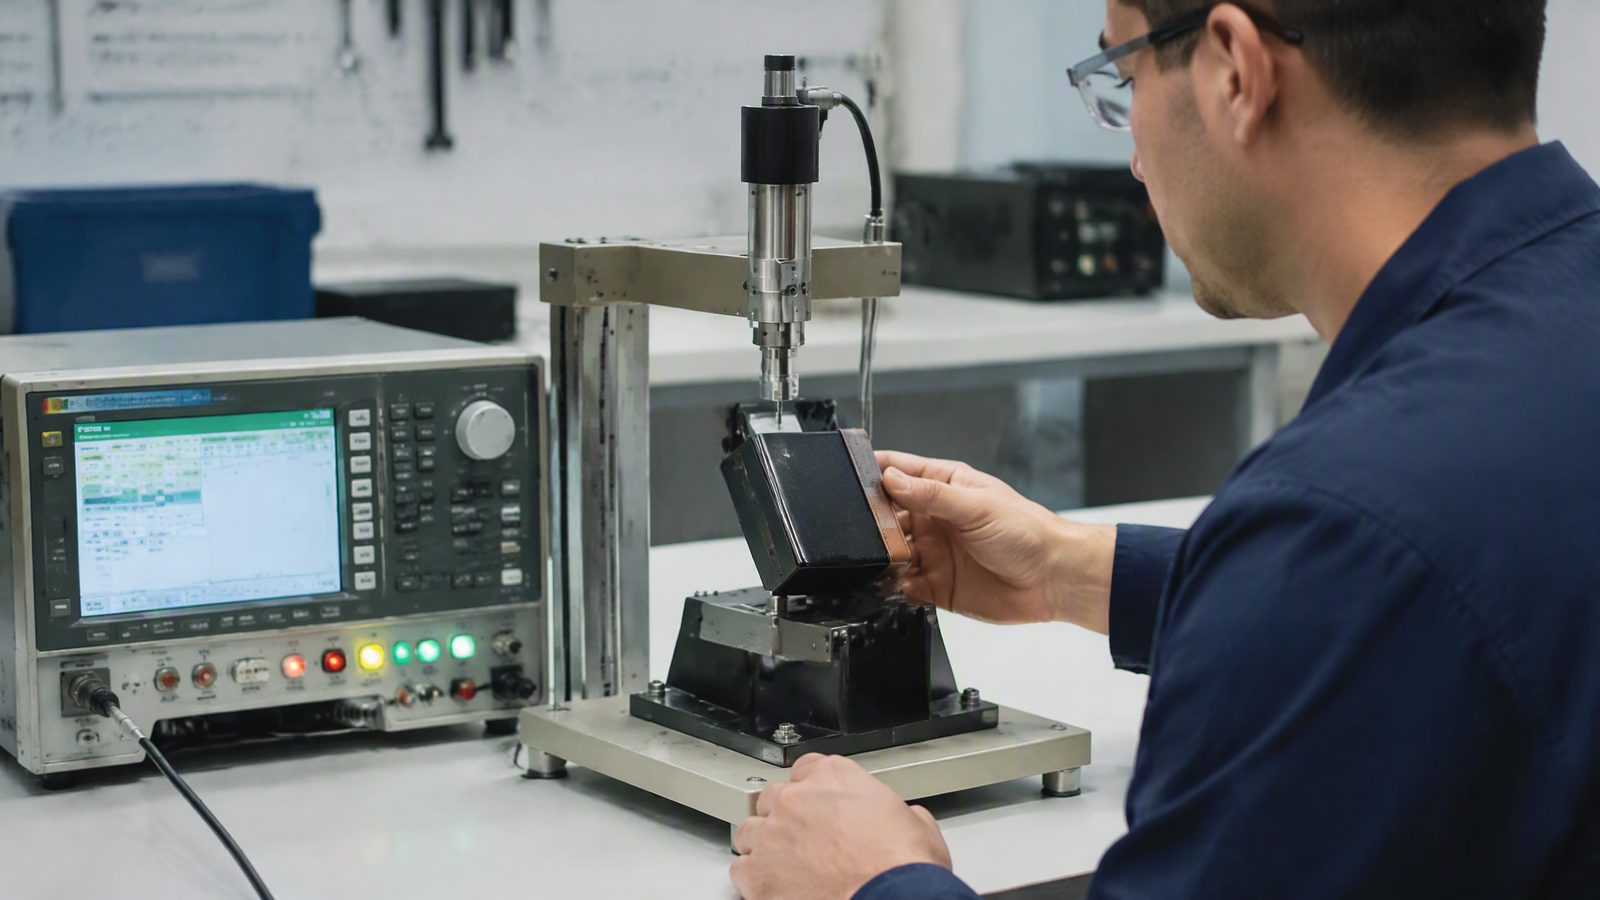
CMM metrology on a first article — every critical dimension is verified against your drawing before bulk starts.
Each machining run is logged with CNC programme version, machine ID, and operator ID. Records are retained for 12 months and can be reviewed with measurement data during a factory visit or video audit.
Tolerance Standards
We publish our internal standards so you can compare them directly with your drawings. If your specification is tighter, we flag it during DFM review and propose a cost-capable process before cutting metal.
| Feature | Our Standard | Industry Typical | Why It Matters |
|---|---|---|---|
| Aluminium shell | ±0.05 mm | ±0.10 mm | Keeps assembly gaps uniform and eliminates blade-like edges |
| Card slot width | ±0.02 mm | ±0.05 mm | Ensures smooth card slide without looseness over time |
| Ejection mechanism | ±0.03 mm | ±0.08 mm | Controls trigger force and repeatability |
| Surface flatness | 0.05 mm | 0.10 mm | Prevents rocking on tables and improves anodising consistency |
| Hole position | ±0.05 mm | ±0.10 mm | Aligns screws, magnets, and mating inserts across batches |
DFM Review Process
Every project starts with a DFM (Design for Manufacturing) review. We do not simply quote your drawing; we analyse it for cost, risk, and assembly logic, then send you a written report with recommended changes.
Your 2D/3D File
Send STEP, IGES, or native CAD. Include material notes, finish callouts, and critical dimensions.
DFM Analysis
Our engineers check wall thickness, undercuts, draft angles, and tolerance stack-up. Red flags are highlighted with photos from past projects.
Material Recommendation
We match the alloy grade to your strength, weight, and anodising goals. If 6061-T6 is overkill, we tell you. Full material grades and surface options are compared on our materials page.
Tooling Strategy
We decide soft-tool vs. hard-tool, multi-cavity layout, and whether a 5-axis operation saves downstream handwork.
FAI Report
First Article Inspection includes CMM data, surface traces, and functional test results before bulk production starts.
CNC & Stamping Equipment
Capacity numbers mean little without context. Below is what our equipment actually lets us do for wallet-level metalwork.
120+ CNC stations
The fleet spans 3-axis workhorses for simple pockets, 4-axis units for angled slots, and 5-axis machines for complex curved shells and undercuts that would otherwise require multiple setups. This reduces fixture error and keeps repeatability within ±0.03 mm on secondary features.
Robotic polishing
Belt speed, pressure, and angle are program-controlled. Compared with hand polishing, robotic cells hold Ra values within a 10% band and eliminate the “good day / bad day” variance that causes colour drift during anodising.
Stamping dies, maintained in-house
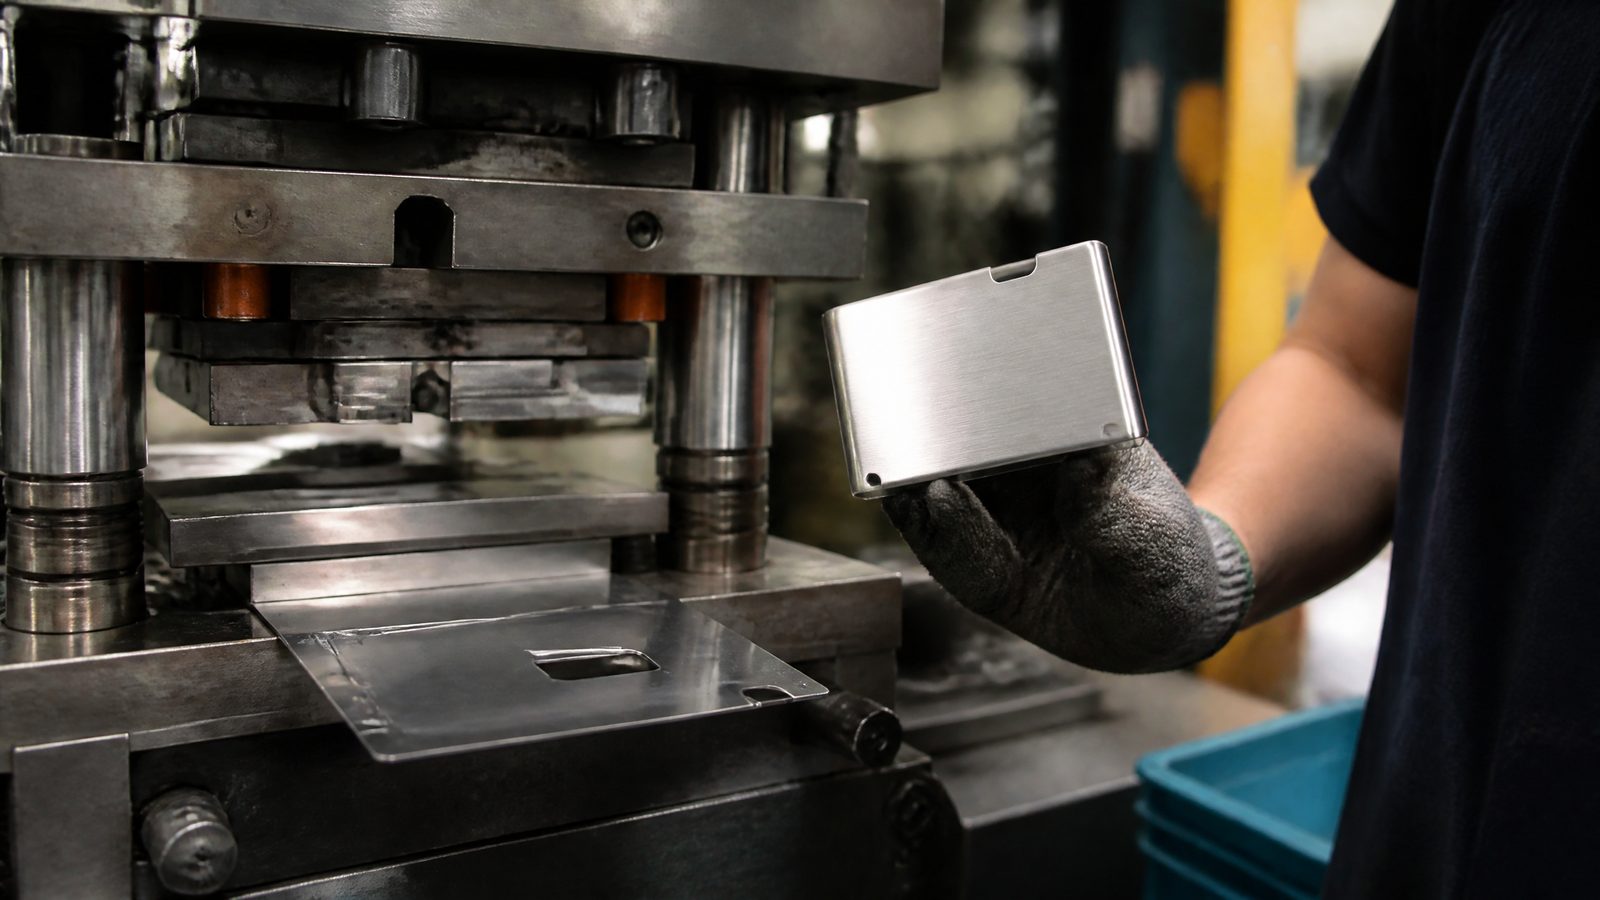
Our toolroom sharpens and repairs dies on site. Die changeover takes under 30 minutes, so we can run small batches without penalising you for setup time.
Surface Preparation
Shot Blasting for Uniform Matte Finish
After stamping, every metal card-shell enters a continuous mesh-belt shot-blasting machine. High-velocity steel shot removes burrs, oxide scale, and machining residue, then roughens the surface to a consistent matte texture. This step is mandatory before anodising or painting; without it, dye adhesion is unpredictable and cosmetic rejects rise sharply.
Ra 0.8–3.2
Surface roughness band delivered consistently across the mesh belt, verified per batch
100%
Every stamped shell is blasted; no skip-lot or visual-only screening
Compressive
Surface peening introduces residual compressive stress, improving fatigue life and spring-back of thin metal plates
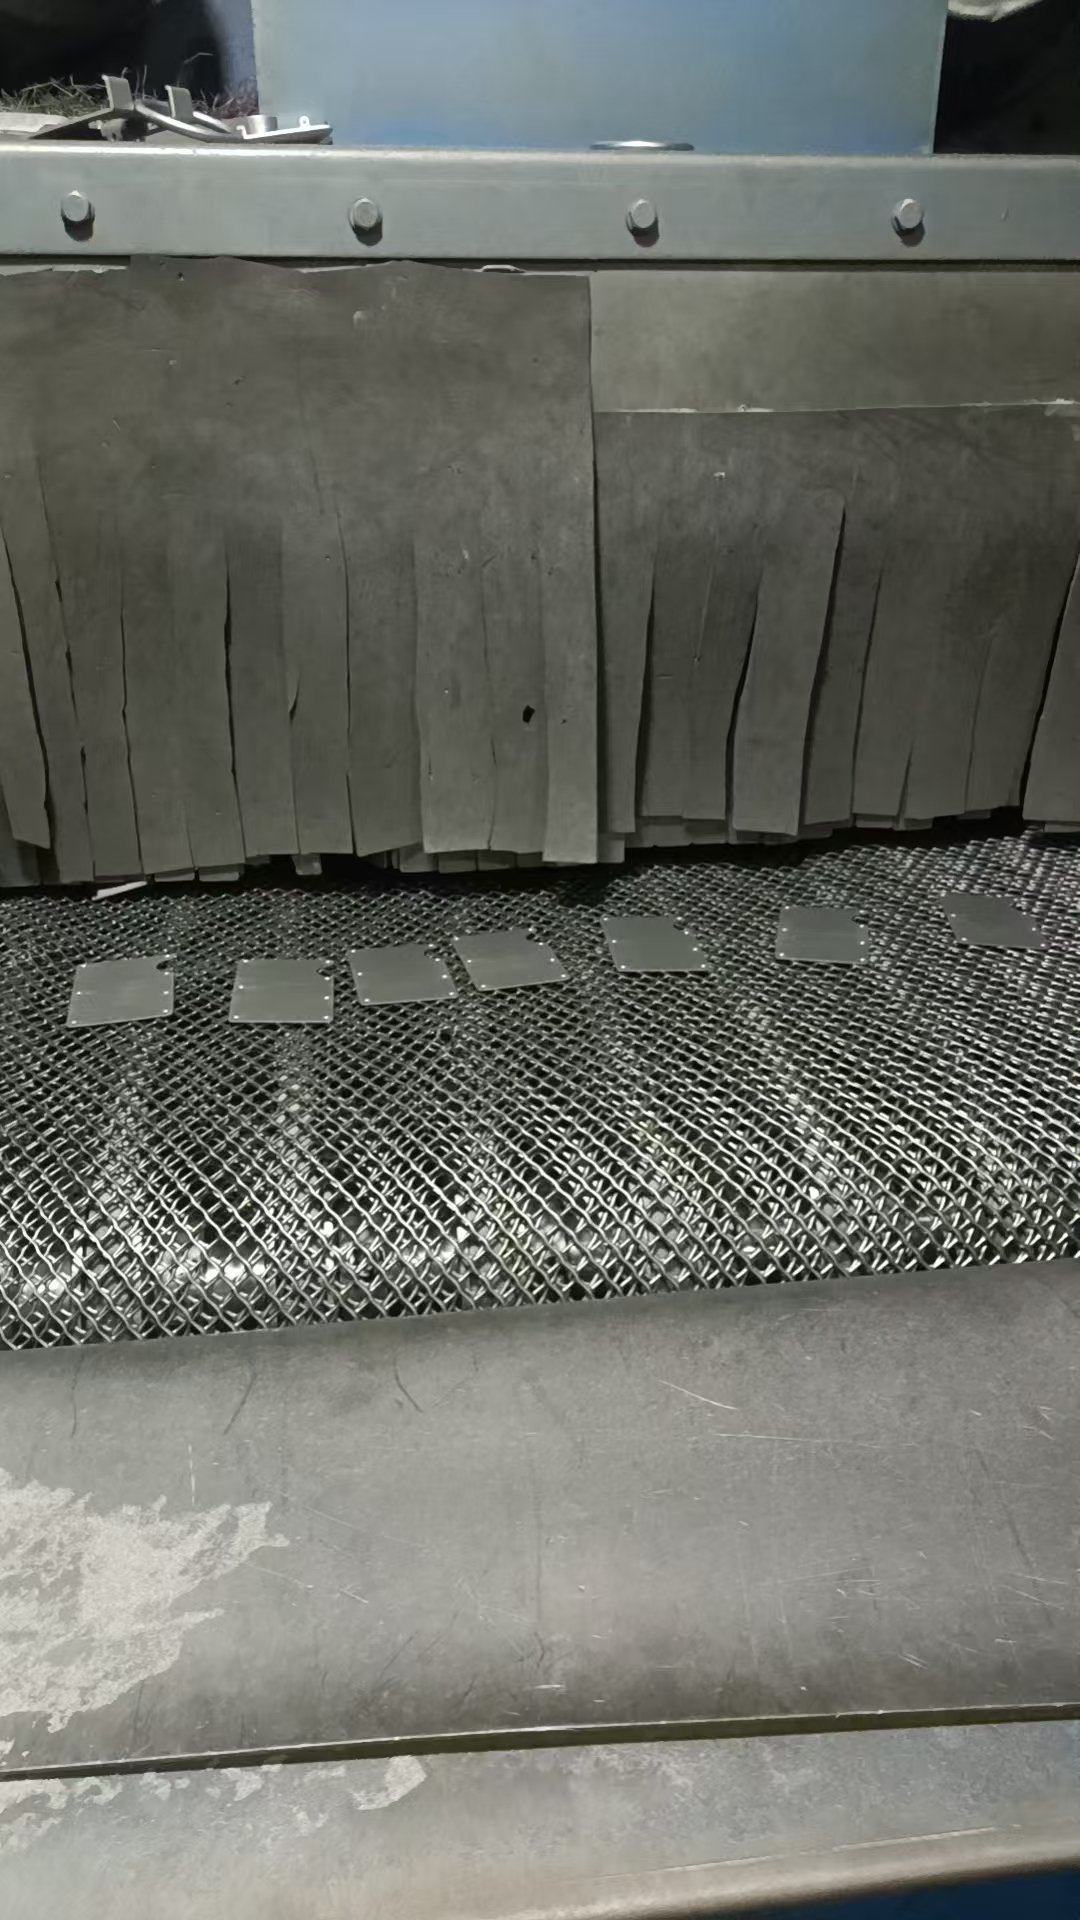
Stamped shells enter the mesh-belt blaster through rubber dust curtains that contain steel shot and dust inside the chamber.
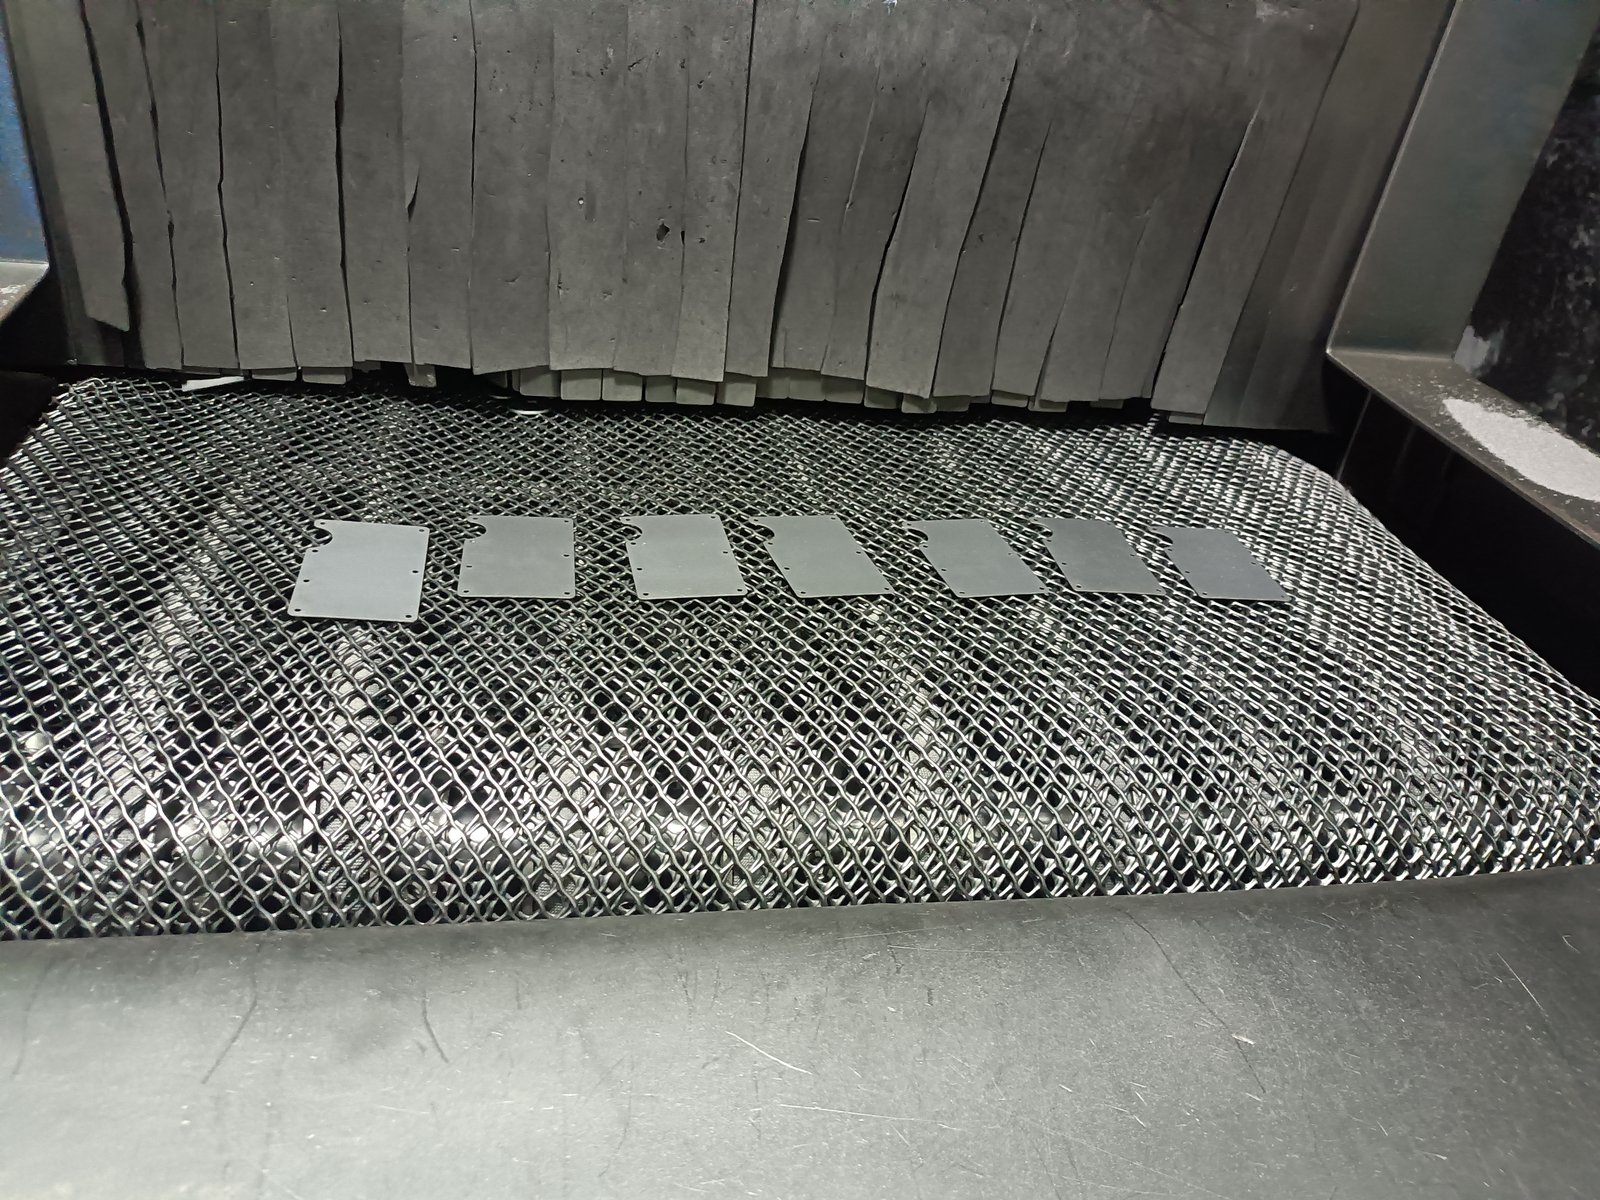
The mesh belt lets shot fall through for recovery while transporting shells at constant speed. 垂帘 (rubber strip curtains) seal the outlet to prevent media escape.
Blasting media, air pressure, and belt speed are recorded per batch. If a later anodising batch shows colour drift, we can trace back to the exact blasting parameters and reproduce the surface condition. For a full comparison of surface finishes after blasting — bead-blast, brushed, anodised, PVD — see the materials and finishing guide.
Surface Finishing
Anodizing for Colour & Corrosion Protection
After shot blasting, aluminium shells move to the anodizing line. Each shell is mounted on a multi-tier rack and immersed in a sulfuric acid electrolyte bath. Anodic oxide grows directly from the base metal, creating a hard, porous layer that accepts organic dye and is then sealed to lock in colour and add corrosion resistance. Unlike paint or PVD, anodized colour is part of the metal itself — it will not chip, flake, or wear through under normal use.
Rack-mounted
Each shell is individually fixtured on a tiered rack to prevent contact marks and ensure uniform current distribution across the entire batch
Type II
Sulfuric acid anodizing for decorative colour and moderate wear resistance on 6061-T6 and similar aluminium grades used in our wallet shells
Dye + Seal
Porous oxide layer is dyed to specification, then sealed in a hot nickel-acetate or deionised water bath to close pores and lock colour
Bath temperature, acid concentration, current density, and dwell time are logged per rack. If a colour batch drifts, we can trace back to the exact bath parameters and adjust before the next load. For colour matching across large orders, we maintain master samples and run small pre-production racks for client approval before bulk anodizing begins. See the materials and finishing guide for a comparison of anodized, PVD, brushed, and bead-blast surfaces.
Measurement & Verification
We trust data over eyes. Every shift starts with gauge calibration, and every first article is fully dimensioned before the operator presses “cycle start” on bulk.
CMM (Coordinate Measuring Machine)
ZeissCONTURA system, accuracy ±0.001 mm. Used for FAI, capability studies, and dispute resolution.
Go / no-go gauges
Custom hard gauges at key dimensions let line inspectors check a part in seconds, not minutes.
Surface roughness tester
Ra 0.4–3.2 µm range, selectable per drawing callout. Results are printed and bonded to the batch traveller.
First Article Inspection (FAI)
A complete FAI package is mandatory for every new part number and every tooling revision. It includes dimensional report, material certificate, and surface finish trace. Bulk production cannot start without your written approval of the FAI. FAI data then feeds the five QC gates that protect every batch.
From Prototype to Bulk Without Re-Tooling
The gap between an approved sample and a production batch is where most wallet projects lose time. We close it with a documented transfer path, so the process that produced your approved prototype is exactly the process that produces your bulk order.
Pre-pilot build (typically 50 units)
Run on the same stations, same fixtures, and same programme files that will be used for bulk. This validates cycle time, rejects, and operator instructions before you commit to hard tooling.
FAI release
The pre-pilot batch is dimensioned 100% and signed off as the frozen reference for bulk. Any later deviation is caught against this baseline, not against a drawing that nobody re-read.
Tooling freeze & programme lock
CNC programmes, die sets, and polishing recipes are version-locked and archived with the batch. A repeat order six months later uses the identical setup, which is why repeat orders typically skip sampling entirely.
If you only need validation before committing to bulk, start with the prototyping programme — three paths from idea to tested sample, each with a fixed timeline and cost.
Typical Projects
We have handled thousands of wallet variants. Here are two representative challenges with real outcomes.
Ultra-Thin Aluminium Shell (0.6 mm Wall)
Challenge: A client needed a pocket-wallet shell at 0.6 mm wall thickness to hit a 35 g target weight. Standard 6061 at this thickness warps during machining and distorts in anodising.
Our Solution: We switched to a harder 7075-T6 variant, added internal rib structures for stiffness, and reduced machining stock to 0.05 mm per side. Tool paths were optimised to minimise clamping stress.
Result: Final shell held ±0.05 mm flatness after anodising. No post-machining straightening was required, and the part passed a 1 m drop test onto concrete.
Complex Card Ejection Mechanism
Challenge: A multi-function design required a curved lever and pinion housing with tight clearance between moving parts. Tolerance stack-up risked either jamming or excessive play.
Our Solution: The curved lever was cut on a 5-axis centre in a single setup to eliminate datum shift. We then ran a 50-piece pre-pilot to refine spring preload and detent geometry before hard tooling.
Result: Mechanism passed 10,000 open-close cycles without wear or force degradation. FAI CMM data showed all clearances within ±0.03 mm of nominal.
Manufacturing detail
Production numbers that hold up
Hard figures for precision machining, capacity and quality control.
FAQ
We prefer STEP, IGES, or SolidWorks files. 2D PDFs with full dimensioning are acceptable for simple parts, but 3D models allow faster undercut and wall-thickness analysis. If your design is sensitive, we can sign an NDA before file transfer.
Standard turnaround is 24 hours for wallet-scale parts. Complex assemblies with multiple components may take 48 hours. Rush reviews can be expedited same-day if the file is clean and complete.
Yes, on specific features. Card slots and bearing bores can be held to ±0.02 mm with dedicated tooling and slower feeds. We will flag which dimensions justify the extra cost and which can remain at ±0.05 mm without affecting function.
We stop production, root-cause the deviation, and submit a corrected FAI at no charge if the error originated in our process. If the drawing or material specification needs revision, we update the DFM and re-quote the adjusted tooling before re-cutting.
See the production line before you commit.
Send us your product idea or a reference sample. A sales engineer will walk you through the relevant stages — tooling, sampling, production and QC — and come back with dates and costs.