
Material Library
Material Grades and Selection
The finish is only half the story — the substrate underneath determines weight, strength, and how well the finish survives daily carry. We stock the grades below in wallet-relevant sheet and plate thicknesses, so your sample material always matches your bulk material.
| Material | Typical Wallet Use | Strength & Weight | Finish Options | Cost Direction |
|---|---|---|---|---|
| 6061-T6 Aluminium | Standard shells, card holders | Good strength-to-weight; best all-round choice | Anodising, sandblast, brush, laser | Baseline |
| 7075-T6 Aluminium | Ultra-thin shells, high-impact designs | ~30% stronger than 6061, similar weight | Anodising, brush, laser | +15–25% |
| 301 Stainless Steel | Slim wallets, clip mechanisms | High spring-back; heavier than aluminium | Brushing, electrophoresis, laser | +20–30% |
| 316 Marine Stainless | Outdoor / saltwater EDC | Corrosion resistance; extra cost for niche value | Brushing, laser | +40–60% |
| Copper Alloy (C1100) | Patina-style retail lines | Dense and heavy; aesthetic-driven choices | Brushing, laser | +10–20% |
| Full-grain Leather | Hybrid wallets, sleeves, refills | Lightweight; pairs with metal frames | Emboss, foil stamp, laser | Varies by tanning |
If you need a grade that is not listed, tell us during quoting — we verify availability and minimum order weight before we commit to a delivery date. Our DFM review flags material changes that would improve cost or durability before tooling starts, rather than after the first sample disappoints you.
Finishing Capability
Surface Finishing That Matches Your Brand
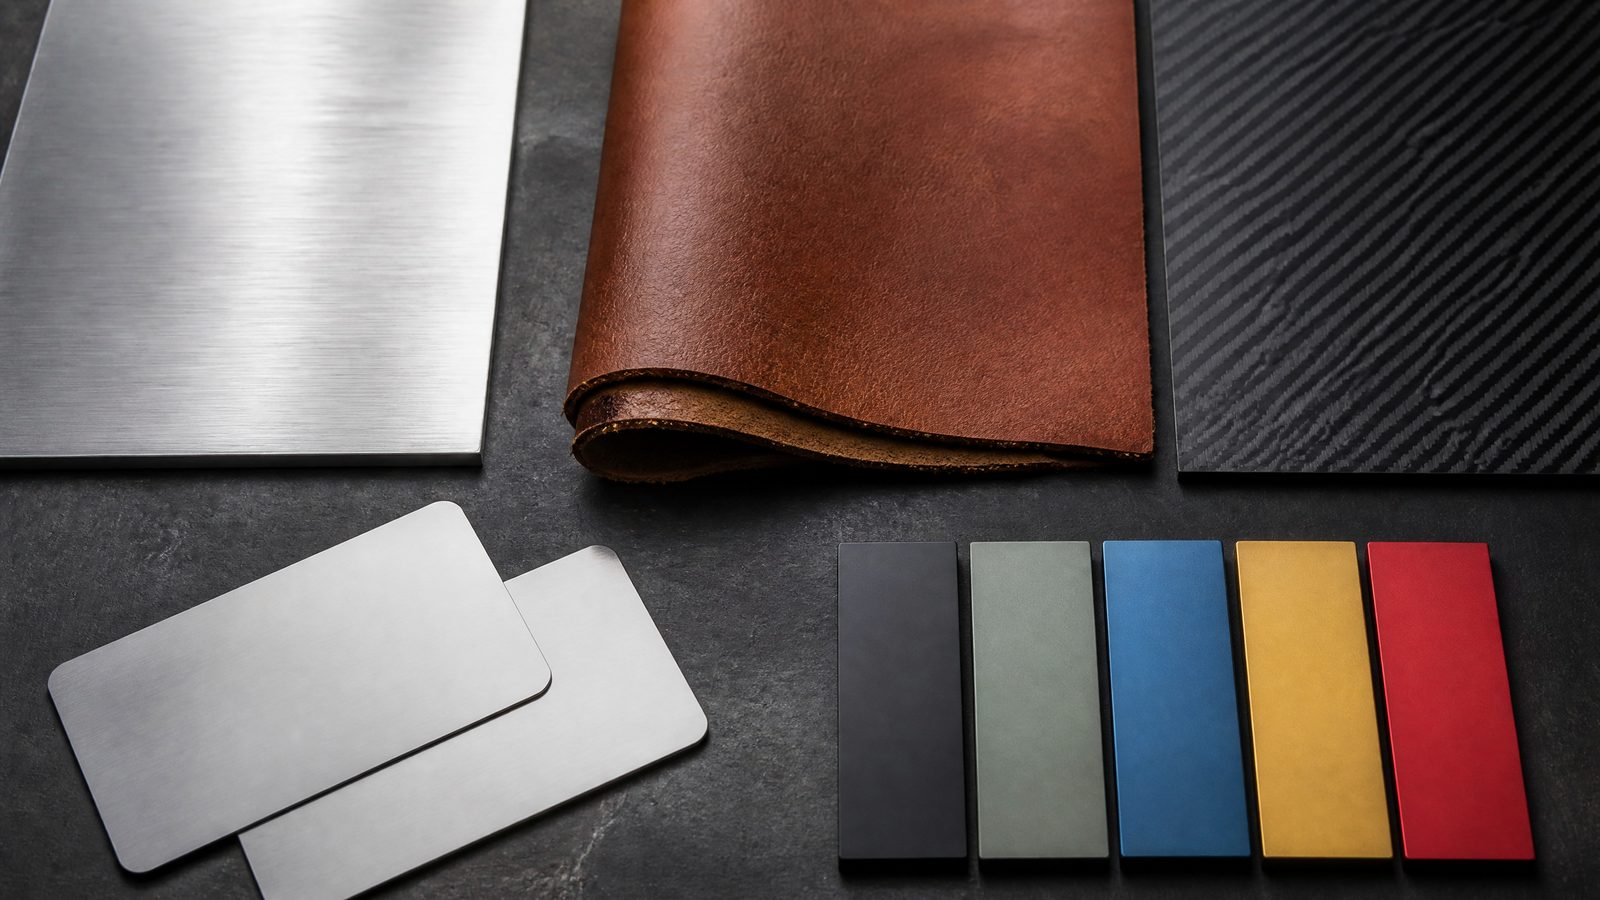
TOPWALLET offers six mainstream finishing processes for EDC wallets, with colour matching to Pantone references or your physical sample. Sample boards are prepared and shipped within 72 hours so you can approve texture and tone before committing to bulk. These finishes are applied across every wallet in the product catalogue and to custom components cut in our machining process.
6
Proven finishes in active production — pick a look your market wants without betting on an untested line
ΔE < 1.5
Batch-to-reference colour match — your reorders look identical to your first run
72 h
Sample board turnaround so you approve texture and tone before tooling is cut
Finish Comparison Table
Use this table to select the right finish for your product line. “Lead time adder” is the extra time beyond base machining. “Cost level” is relative to raw machined aluminium.
| Finish | Appearance | Durability | Best Material | Lead Time Adder | Cost Level |
|---|---|---|---|---|---|
| Anodising (Type II) | Matte to satin; dyeable in colours | Hard oxide layer; good scratch resistance | Aluminium (6061, 7075) | +2–3 days | Medium |
| Sandblasting | Uniform matte; hides tool marks | No added film; depends on base material | Aluminium, Stainless steel | +0.5 days | Low |
| Brushing | Directional hairline texture | Scratches show less due to grain direction | Aluminium, Stainless steel, Copper | +1 day | Low–Medium |
| Electrophoresis | Smooth, even film; opaque colours | Excellent corrosion resistance | Stainless steel, Aluminium | +3–4 days | Medium–High |
| Laser Engraving | Permanent mark; no added layer | Indelible; does not wear off | Aluminium, Stainless steel, Copper, Leather | +0.5 days | Low (per unit) |
Colour Matching Process
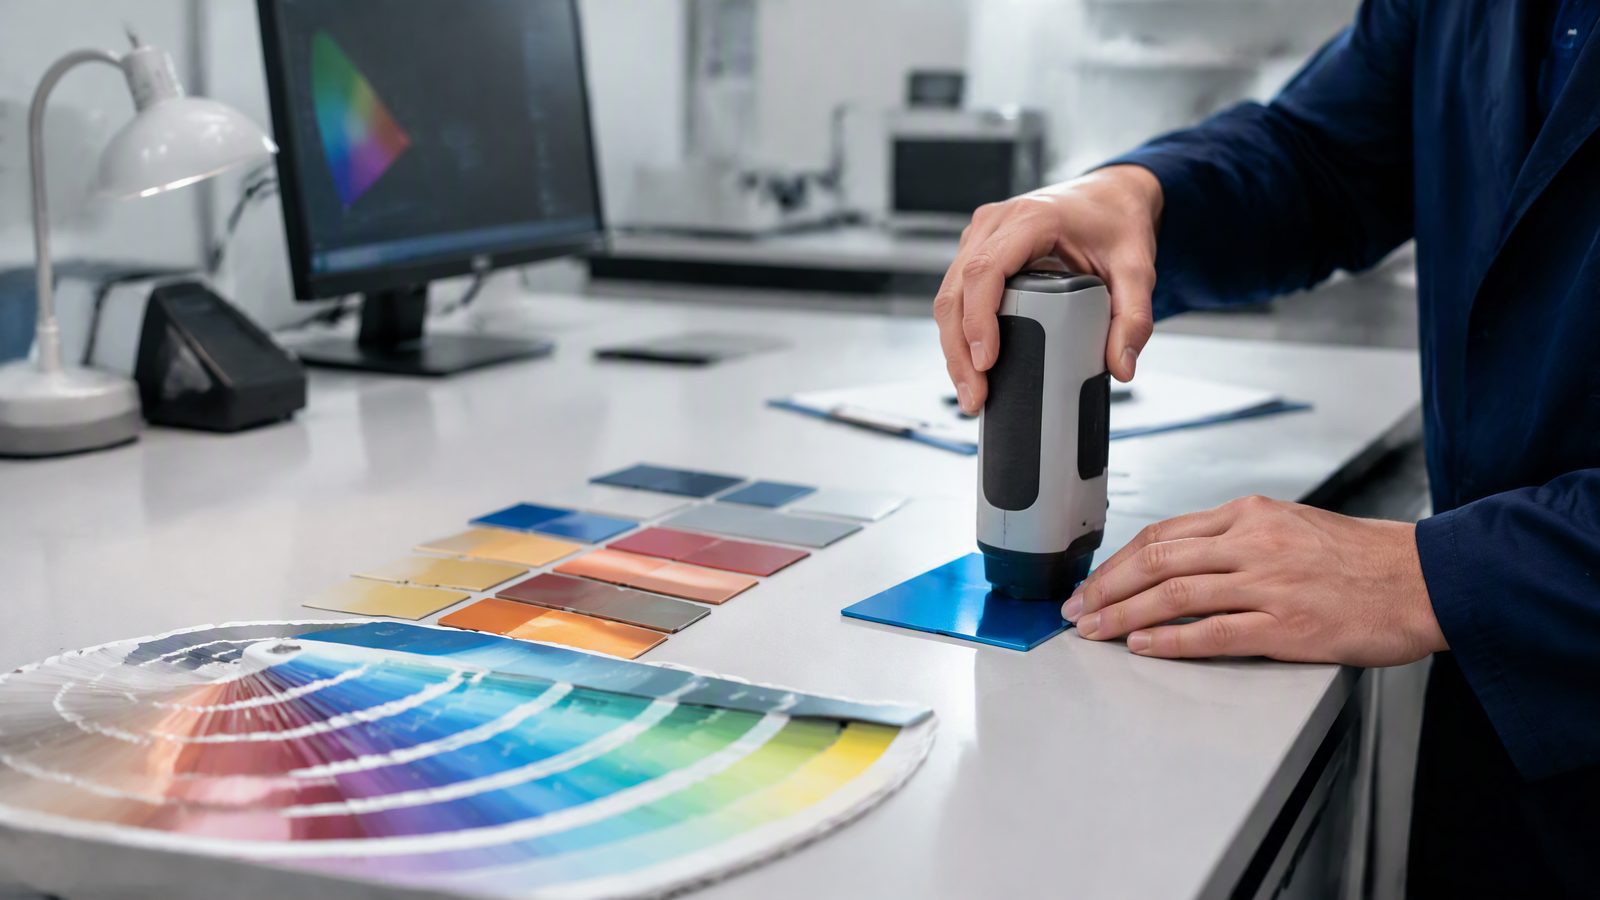
We do not guess colour. Our lab uses spectrophotometry to map your reference to a reproducible formula, then locks it into the production traveller so batch 50 looks identical to batch 1.
Reference Sample
You send a physical swatch, Pantone code, or competitor part. We store it in a light-controlled cabinet.
Lab Analysis
Our spectrophotometer reads L*a*b* values and formulates a dye or paint mix. For anodising, we map to a proprietary dye curve.
Test Panel
A 100 mm × 100 mm panel is processed on the exact line that will run your bulk. This eliminates line-to-line variance.
Your Approval
You sign off the panel or request a tweak. We allow up to three iteration cycles at no charge.
Production Batch
The approved formula is logged with a unique batch ID. Colour tolerance is held to ΔE < 1.5 versus the master panel.
Approved dye formulas are logged against a unique batch ID with the bath, temperature, and duration recorded on the production traveller. Colour is recalled by batch ID on reorder, not by memory.
Durability Testing
Finishes are tested to industry standards before they enter our standard offering. If your market requires a non-standard test, we can add it to the control plan.
| Test | Method | Standard | Our Result |
|---|---|---|---|
| Abrasion | Taber abraser, CS-17 wheel, 1 kg load | ASTM D4060 | No substrate exposure after 500 cycles on anodised aluminium |
| Salt spray | 5% NaCl, 35 °C, continuous | ASTM B117 | No corrosion on sealed anodising after 96 hours |
| Cross-hatch adhesion | 1 mm grid, 3M 610 tape pull | ASTM D3359 | Rating 5B (0% peel) on electrophoresis coating |
| Colour difference | Spectrophotometer, D65 illuminant | CIE ΔE 2000 | ΔE < 1.5 between batch and master panel |
Material Compatibility
Not every finish works on every substrate. Below is our approved matrix for wallet-grade materials.
Aluminium
Anodising (Type II), sandblasting, brushing, laser engraving. Best overall versatility for lightweight wallets.
Stainless steel
Electrophoresis, brushing, laser engraving. Anodising is not recommended because stainless does not form a porous oxide layer suitable for dye absorption.
Copper
Brushing and laser engraving only. We do not recommend anodising copper for wallet applications; the oxide layer is soft and discolours quickly with skin contact.
Leather
Embossing, foil stamping (hot stamping), and laser engraving. We can match grain patterns to your reference hide and deboss logos to a depth of 0.3 mm.
Not sure which finish fits your price point and retail channel? Our OEM / ODM team recommends material-finish combinations before you commit to tooling, based on the same matrix above.
Sample Board Service
Approving a finish from a photograph is risky. Our sample board program lets you feel the texture and check the colour under your own lighting before tooling is committed.
72-hour dispatch
From receipt of your reference or Pantone code, we produce a labelled board and ship by express courier.
Complete process library
The board includes all six finishes on the material you specify, plus one laser-engraved logo sample if artwork is provided.
12-month traceability
We archive the formulation and retain a physical retention sample for one year. If you reorder, the colour is recalled by batch ID, not memory.
Manufacturing detail
Material facts for sourcing decisions
Grades, colours, finishes and durability data to help you specify the right wallet.
FAQ
Yes. We match to Pantone coated/uncoated codes or physical samples. Our lab targets ΔE < 1.5, which is indistinguishable to the human eye under standard viewing conditions. Metallic or pearlescent colours may require a longer matching cycle.
Type II anodising on aluminium offers the best balance of scratch resistance and cost for EDC wallets. The hard oxide layer withstands keys and coins better than bare metal. For extreme abrasion resistance, electrophoresis on stainless steel can be specified, though it adds cost and weight.
We can produce glossy anodising and high-gloss electrophoresis on request. Gloss levels are specified in GU (gloss units) at 60°. Typical wallet finishes are matte or satin (5–15 GU), but we can target 80+ GU for a mirror-like appearance if your design calls for it.
Yes. Common combinations include brushed aluminium with laser-engraved logos, or sandblasted bodies with polished chamfers. We mask areas precisely to prevent process crossover. Combining two finishes usually adds one day to lead time.
For most first orders, 6061-T6 aluminium with Type II anodising is the safest baseline: proven supply, predictable cost, and a wide colour range. Reserve 301 stainless steel for spring-loaded mechanisms and 7075 for ultra-thin designs where every gram counts. Tell us your target price point and market, and the DFM review will propose the most cost-effective grade that survives real EDC use.
Yes. Sample boards and prototypes are produced from the same stocked lots used for bulk production. The substrate, dye formula, and line settings are recorded against the batch ID, so what you approve at sampling stage is exactly what ships at scale.
See the production line before you commit.
Send us your product idea or a reference sample. A sales engineer will walk you through the relevant stages — tooling, sampling, production and QC — and come back with dates and costs.